When rebuilding engines, achieving a precise crosshatch finish and clean bore edges is essential for optimal oil retention and piston ring seating. This guide highlights top 4 inch cylinder ball hone tools and similar oversized, ball-style hones designed to size, deburr, and refine cylinder bores. Each pick emphasizes self-centering action, durable silicon carbide abrasives, and compatibility with common drill setups. Use this overview to compare finishing performance, bore compatibility, and ease of use for automotive, hydraulic, and pneumatic cylinders.
Summary table of selected products:
| Product | Brand | Diameter | Grit | Key Benefit |
|---|---|---|---|---|
| ZXQDRE 4 Inch Cylinder Hone Tool | ZXQDRE | 4 inch | 240 | Self-centering, fast deburring, crosshatch finish |
| Brush Research GB41824 FLEX-HONE | Flex-Hone | 4-1/8 inch | 240 | Oversized design for self-centering, versatile finish |
| Brush Research GBD40024 FLEX-HONE | Flex-Hone | 4 inch | 240 | Crosshatch finish, durable USA-made |
| Cylinder Hone, 240 Grit Silicon Carbide (4-1/8″) | FIMXSD | 4-1/8 inch | 240 | Deburring and finishing, compatible with various spindles |
| Cylinder Honing Ball Brushes 4.125″ (105mm) | xvierut | 4.125 inch | 240 | Flexible ball-style for self-centering honing |
ZXQDRE 4 Inch Cylinder Hone Tool Overview
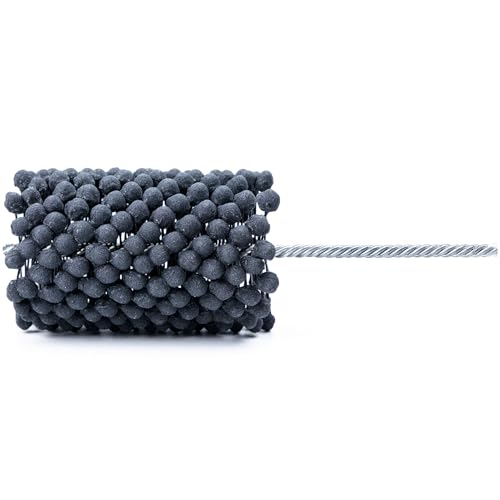
The ZXQDRE 4 Inch Cylinder Hone Tool provides a robust option for engine rebuilding, delivering a crosshatch finish known for improved oil retention. The 240 grit silicon carbide abrasive is suitable for mild steel, stainless steel, and cast iron, producing a smooth Ra in the range of 24-32 for bore refinishing. A notable feature is its self-centering and aligning design, which maintains consistent contact pressure across the bore wall, ensuring uniform results. This tool also deburrs cross holes in a single step, increasing workflow efficiency when restoring engine cylinders and related hydraulic components.
Key features include self-centering operation and a design optimized to evenly press the abrasive against the bore. The combination of finishing and deburring in one step reduces setup time and minimizes additional passes. This makes it suitable for engine blocks, brake master cylinders, and similar components where a reliable crosshatch finish is critical.
Compatibility and usage notes: pair this hone with standard rotating spindles, including handheld drills or drill presses. The tool’s oversized configuration helps maintain alignment as it travels through the bore, reducing the risk of uneven wear or gouging. While designed for core automotive metals, it also serves hydraulic and pneumatic cylinder maintenance tasks where a precise surface finish is essential.
Brush Research FLEX-HONE 4-1/8″ (GB41824) Review

The FLEX-HONE GB41824 is a trusted, USA-made option that emphasizes an intentionally oversized construction to optimize cylinder pressure, enabling self-centering and self-aligning behavior. The 240 grit silicon carbide abrasive produces a reliable crosshatch finish across mild steel, stainless steel, cast iron, and other softer ferrous materials. This tool is widely used for rebuilding hydraulic and pneumatic cylinders, engine bores, valve guides, and related components. Its durability and consistent finish profile make it a popular choice among professionals and automotive enthusiasts alike.
Design advantages include the oversized head that adapts to bore contours and wear, maintaining pressure consistency for uniform results. The flexible, ball-shaped abrasive arrangement allows for controlled removal of minor imperfections while preserving bore geometry. The GB41824 is compatible with a range of spindles and is frequently used where a precise surface finish is a prerequisite for reliable piston sealing and oil retention.
Brush Research GBD40024 FLEX-HONE 4″ 240 Grit

The GBD40024 FLEX-HONE shares the same design philosophy as other FLEX-HONE products, offering a self-centering, self-aligning system that helps achieve a clean crosshatch finish. The tool’s 4-inch diameter and 240 grit silicon carbide abrasives are well-suited for engines and hydraulic components made from mild steel, stainless steel, or cast iron. This model emphasizes American manufacturing quality and control, ensuring a consistent finish while reducing the risk of bore distortion during honing operations.
Use cases include engine cylinder refurbishment, brake cylinder preparation, and hydraulic component restoration. The oversized nature improves bore contact pressure distribution, while the ball-style abrasive arrangement helps to minimize gouging and produce a uniform surface. With standard drill compatibility, it’s a practical choice for shops and DIY enthusiasts working on automotive and industrial projects.
Cylinder Hone 240 Grit Silicon Carbide 4-1/8″ (FIMXSD)

This 4-1/8″ cylinder hone from FIMXSD uses a 240-grit silicon carbide abrasive to deliver a self-centering, self-aligning honing action. It is designed for bore diameters from 3.751″ to 4.125″ and features an abrasive length of 4″, a 0.31″ shank, and an overall length of 13.5″. The tool is capable of finishing and deburring, compatible with various rotating spindles ranging from hand drills to CNC equipment. It targets softer ferromagnetic materials like aluminum, brass, bronze, and low-carbon steel, as well as cast iron, delivering a 24–32 microinch surface finish that supports efficient piston ring seating and improved compression.
Practical benefits include reliable self-centering behavior, reduced setup time, and broad compatibility with different machines. This makes the FIMXSD hone a versatile choice for automotive engine work, hydraulic cylinder maintenance, and industrial equipment maintenance where a consistent crosshatch pattern aids performance and longevity.
Cylinder Honing Ball Brushes 4.125″ By xvierut

These cylinder honing ball brushes from xvierut are designed to complement bore finishing with a flexible rubber-centered design that fits bore sizes around 4.125 inches. The abrasive is silicon carbide at 240 grit, providing effective removal of light burrs and surface imperfections to achieve a smoother cross-sectional finish. The kit is useful for hydraulic and pneumatic cylinder refurbishment, engine bores, brake cylinders, and related components where consistent cross-hatch texture improves oil retention and ring sealing.
Key considerations include bore-size compatibility, overall honing length, and shank compatibility with existing rotating spindles. The flexible ball-brush approach reduces the risk of over-machining delicate areas while delivering a uniform final surface. This option is especially suitable for technicians who need a versatile, adaptable tool that can work with a variety of spindle speeds and machine types.
Buying Guide: Key Purchase Considerations
- Bore diameter compatibility: Confirm the tool’s compatible bore range matches your cylinders (common ranges include 3.75″–4.13″ and similar).
- Abrasive grit and finish: 240 grit is a common choice for engine bores, delivering crosshatch patterns that aid oil retention. Higher grit (e.g., 320) can yield finer finishes for specific components.
- Self-centering design: Oversized or ball-style hones centered inside the bore reduce tapering and ensure uniform contact pressure for consistent finishes.
- Material compatibility: Most tools are suitable for mild steel, stainless steel, cast iron, and other ferrous alloys. Verify compatibility with your target material.
- Versatility: Some hones also deburr holes and cross holes, reducing steps in the workflow. Consider whether you need deburring in addition to honing.
- Spindle compatibility: Check that the tool can be chucked into standard rotating spindles, including handheld drills and drill presses, or CNC equipment as needed.
- Durability and origin: USA-made options often emphasize consistent quality and long-term durability, which may matter for professional shops.
- Maintenance and safety: Follow manufacturer guidelines for feed pressure and speed to avoid over-honing or overheating the bore.
Additional Considerations: Perspectives And Use-Cases
Engine builders often prioritize crosshatch quality and oil retention, especially in rebuilds where new piston rings must seat quickly. For hydraulic and pneumatic cylinders, uniform crosshatch and deburring quality contribute to smoother hydraulic action and longer service life. In shop settings, the choice between different diameters and grits may hinge on available spindle tooling, bore tolerances, and the desired balance between speed and finish quality. Flexible ball-hone brushes provide an alternative approach for challenging bore geometries or tight tolerances, offering controlled material removal while preserving bore integrity.
For DIY enthusiasts, selecting a tool sized near the target bore with a compatible spindle is often sufficient. In professional environments, investing in a USA-made option with proven consistency can reduce rework and ensure repeatable results across multiple jobs. When comparing products, evaluate not only the initial cost but also the expected life of the abrasive, the ease of achieving a repeatable finish, and the availability of compatible accessories or replacement abrasives.